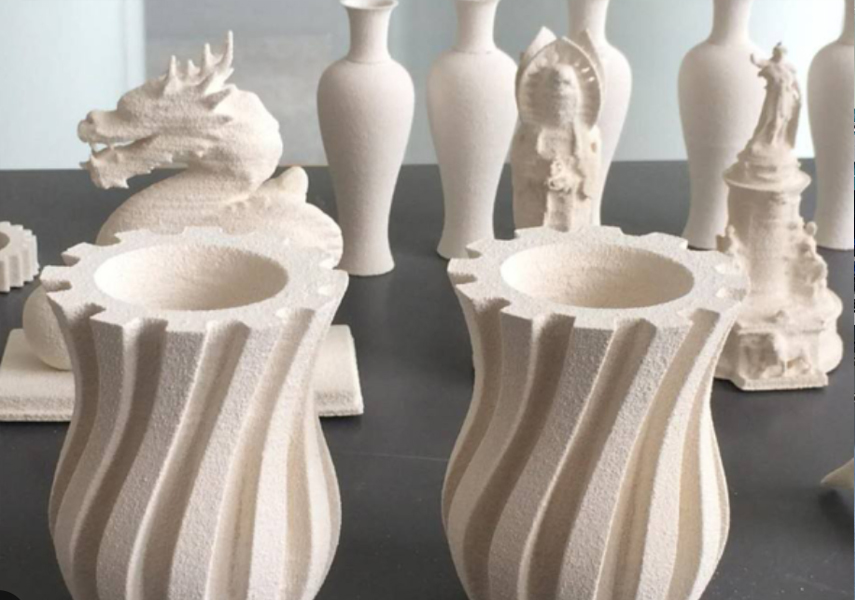
Innovation in art-ceramic powders is fundamentally about turning form, color, texture and firing response into controllable design parameters.Future differentiation in art ceramics will therefore come not only from craftsmanship, but also from material engineering that makes complex artistic effects repeatable and manufacturable.
Eco-friendly ceramic additives should deliver more than a sustainability label. Their real purpose is to achieve the required ceramic performance with less firing energy, fewer virgin resources or additional environmental functionality.The best solution is therefore the one that improves sustainability without sacrificing manufacturing stability or product life.
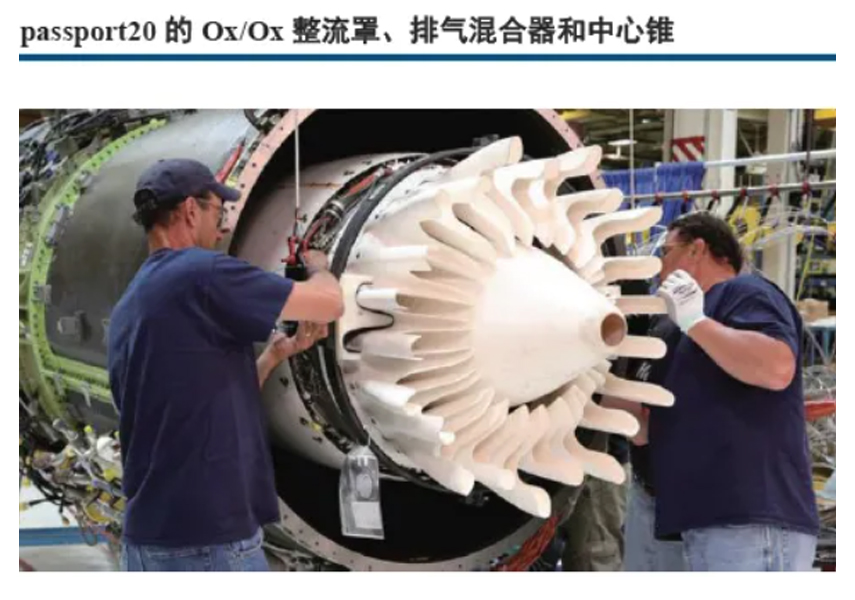
The aerospace value of ceramic powders goes beyond heat resistance. They support higher operating temperatures, lower structural weight, oxidation resistance and more complex component geometries.The next competitive advantage will come from producing powders with consistent chemistry, particle characteristics and processing behavior rather than simply offering a recognized ceramic composition.
The purpose of additives in medical ceramics is to control processing, microstructure and functional phase stability with high precision. A suitable additive system must therefore be evaluated through the complete manufacturing route—from slurry preparation and forming to debinding, sintering and final material testing.
The role of ceramics in new energy is shifting from passive heat-resistant materials to functional materials responsible for safety, ion transport, insulation and thermal management.Future ceramic raw-material competitiveness will therefore depend not only on purity, but also on precise control of particle size, phase composition, interfaces and batch consistency.
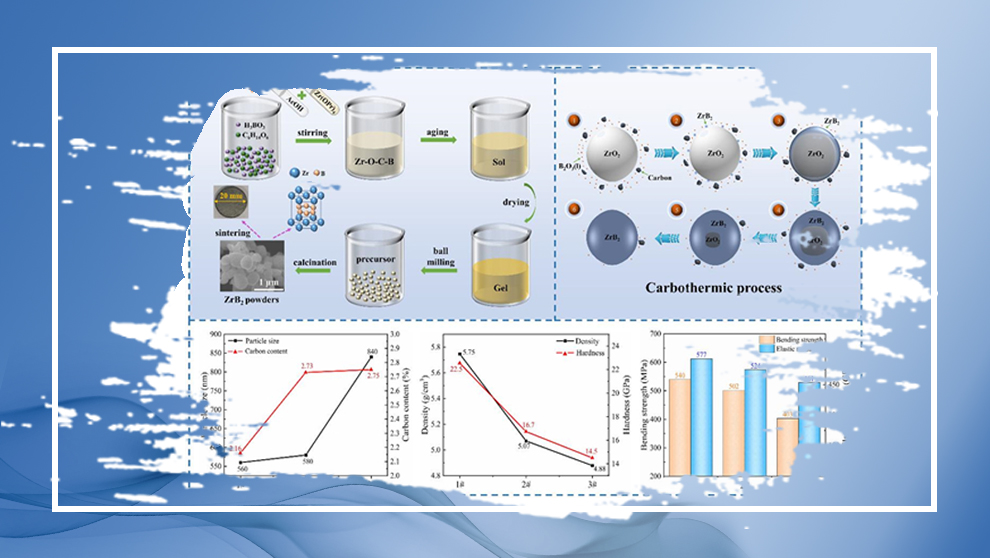
The future of advanced ceramic powders is not simply nanoscale powder production. It is the coordinated control of purity, particle size, morphology, dispersion and sintering activity.The competitive advantage is increasingly shifting from possessing a ceramic composition to producing a highly consistent powder engineered for a specific forming, printing and sintering process.
The real value of additives in building ceramics is to widen the stable manufacturing window. A good additive system improves slurry preparation, pressing or glazing at the lowest effective dosage without creating additional firing defects or unnecessary cost.
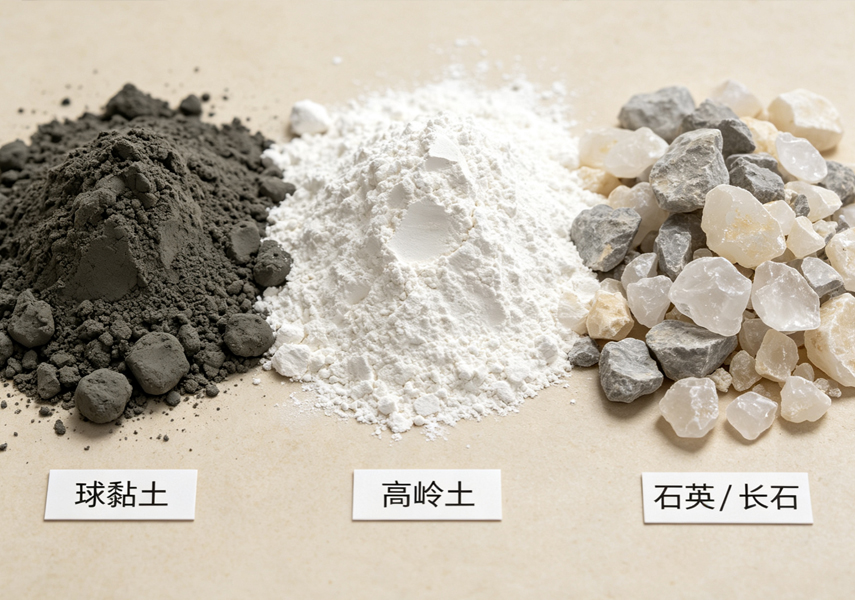
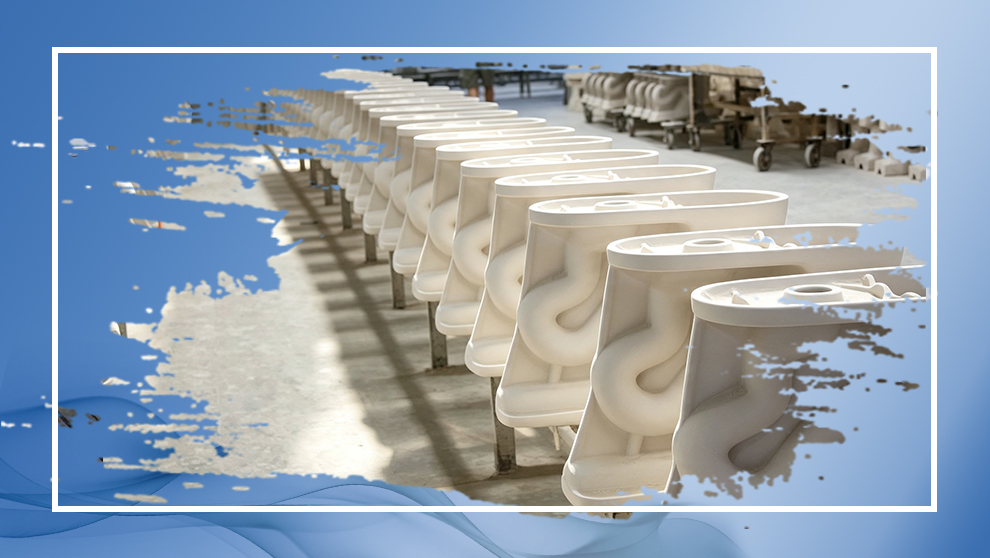
A sanitary ceramic recipe is not defined by one universal percentage. Clay enables forming, quartz stabilizes dimensions and feldspar drives densification. When raw-material sources change, slurry behavior, shrinkage and the firing window should be revalidated before production.
A ceramic powder sintering study should establish the relationship between temperature, shrinkage, density and porosity. Reliable conclusions require controlled green density, standardized firing and repeat testing. The best powder is not merely the one that reaches the highest density, but the one that provides a stable and manufacturable sintering window.
Additive stability is not simply the absence of visible deterioration during storage. A stable additive must still control dispersion, flow, forming and burnout after aging. Combining storage observation, rheology, sedimentation testing and thermal analysis provides a practical basis for setting shelf life, incoming-inspection limits and a reliable processing window.
Laboratory formulation optimization uses structured experiments to replace uncontrolled trial and error. The practical sequence is to define performance limits, screen components, model composition–property relationships and verify the optimum through repeated and pilot-scale trials. The best formulation is not simply the strongest or lowest-absorption sample; it is the composition that remains stable, manufacturable and economical across realistic production conditions.
Additives often affect ceramic testing indirectly through porosity, grain size, secondary phases and residual defects. Improvement in one measured value does not prove that overall performance has improved. Reliable evaluation should connect additive dosage, processing history, microstructure and test results rather than selecting only the most favorable data.
The purpose of ceramic raw-material analysis is not to use the most expensive instrument. It is to select the correct method for the manufacturing question. XRF provides routine major-element control, ICP measures trace impurities, XRD identifies mineral phases and loss on ignition evaluates volatile components. Only when representative sampling, standardized preparation, instrumental analysis and production validation are connected can laboratory data support stable formulations and repeatable ceramic quality.
Electronic-component manufacturing requires ceramic raw materials that deliver repeatable functional performance, not merely successful sintering. Reliability depends on controlling powder chemistry, particle size, densification and microstructure closely enough to keep electrical, thermal, dielectric, piezoelectric or magnetic behavior stable from batch to batch.
The objective of batch consistency analysis is early detection of raw-material drift. Chemical composition, particle size and production-performance data should be placed on the same timeline rather than reviewed as isolated certificates.A supplier should therefore be evaluated not only by whether each lot passes, but by how consistently its material reproduces the same manufacturing behavior over time.
No single measurement fully describes ceramic powder dispersion. Viscosity measures flow, zeta potential describes particle interactions, sedimentation tests stability over time and particle size reveals agglomeration. Combining these methods provides a practical way to identify the optimum dispersant dosage and a stable slurry-processing window.
Effective impurity control is primarily about consistency. A factory should identify which impurities affect its products, measure them with appropriate methods and connect chemical variation with firing performance. This prevents small raw-material changes from becoming visible color, dimensional or yield problems.
Mixing equipment cannot correct poor sampling, scale drift or segregation after blending. Reliable production connects supplier control, separated storage, pre-blending, representative sampling, mixing validation and statistical monitoring so that a batch is not only acceptable on average, but sufficiently consistent throughout.
The purpose of ceramic powder testing is not to generate isolated laboratory values. It is to establish a relationship between powder properties, processing behavior and final quality. Particle size controls packing, surface area controls interfacial activity, density controls filling efficiency and flowability controls feeding stability.
Fine, highly plastic materials such as ball clay and bentonite improve forming behavior and green strength, but they normally require more water and can increase shrinkage and drying time. Lower-plasticity materials such as kaolin, quartz and calcined grog can reduce shrinkage, but excessive additions may reduce workability and dry strength.